Call us now :08071790308
 Send Inquiry

 Send Inquiry
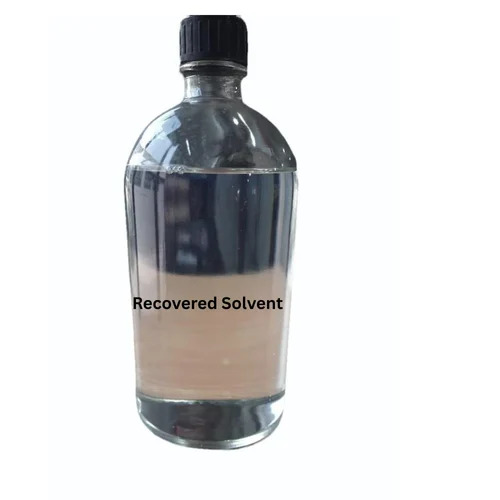
99% Industrial Grade Recovered Solvent
MOQ : 100 Kilograms
99% Industrial Grade Recovered Solvent Specification
- Poisonous
- Yes
- Storage
- Store in cool, dry, well-ventilated area, away from heat/open flames
- Purity
- 99%
- HS Code
- 38140010
- Boiling point
- Range 60C - 130C (depends on recovered composition)
- Molecular Formula
- Mixture of Organic Compounds
- Solubility
- Miscible with most organic solvents
- Smell
- Characteristic, Pungent
- Structural Formula
- Varies (mixture)
- Density
- 0.82 Gram per cubic centimeter(g/cm3)
- Form
- Liquid
- Shape
- Liquid
- Other Names
- Recovered Thinner, Recovered Mix Solvent
- Classification
- Organic Solvent
- Chemical Name
- Recovered Solvent
- Grade
- 99% Industrial Grade
- Standard
- Industrial Standard
- Type
- Industrial Grade Solvent
- Usage
- Industrial
- Main Material
- Recovered Mixed Solvents
- Application
- Paint and Coating Industry, Thinner, Cleaning, Chemical Processing
- Non Toxic
- Yes
- Packaging
- Available in Drum, Tanker or as per customer requirement
- Stability
- Stable under recommended storage conditions
- Transport Regulation
- Classified as Dangerous Goods
- Insoluble Matter
- Negligible
- Water Content
- <1%
- Flash Point
- Below 21C
- Evaporation Rate
- Fast
- Environmental Regulations
- Subject to local environmental and safety regulations
- Compatibility
- Compatible with most organic systems
- Appearance
- Clear to slightly colored transparent liquid
99% Industrial Grade Recovered Solvent Trade Information
- Minimum Order Quantity
- 100 Kilograms
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10000 Kilograms Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
99% Industrial Grade Recovered Solvent About
Experience matchless performance with our 99% Industrial Grade Recovered Solvent-a fresh, high-purity solution offering grandiose utility and exceptional compatibility. Its clear to slightly colored transparent appearance, rapid evaporation rate, and reduced insoluble matter make it ideal for demanding industrial settings. Glorious adaptability to most organic systems ensures access to diverse applications, including paint and coating industries, cleaning, and chemical processes. Rigorously compliant with local environmental and safety regulations, this solvent is available in drums, tankers, or custom packaging to suit every operational need. Choose quality, choose reliability.
Wide-Ranging Applications for Industrial Excellence
Our 99% Industrial Grade Recovered Solvent is suitable for both general and specific uses within the paint and coating industry, acting as a powerful thinner or cleaning agent in chemical processing. Its broad compatibility makes it ideal for fresh projects requiring reduced impurities and rapid drying. Whether you're tackling grand industrial cleanups or nuanced applications in manufacturing, this product provides matchless performance and dependability in every scenario.
Domestic Market Support and Reliable Delivery
Serving the grandiose domestic market, we back every order with legitimate certifications and offer sample availability to ensure satisfaction before bulk commitment. Our efficient dispatching process, aided by specialized transport services, guarantees your order completion is timely and secure. Whether you need drums or tankers, rest assured of a seamless journey from placement to delivery, with each batch dispatched in accordance with industry standards for dangerous goods transport.
FAQ's of 99% Industrial Grade Recovered Solvent:
Q: How should the 99% Industrial Grade Recovered Solvent be stored safely?
A: The solvent should be stored in a cool, dry, and well-ventilated area, away from heat sources and open flames, to maintain stability and safety.Q: What are the main benefits of using this recovered solvent in industrial applications?
A: This solvent offers matchless purity, reduced insoluble matter, fast evaporation, and compatibility with most organic systems, making it especially effective and versatile in various industrial applications.Q: Where can the 99% Industrial Grade Recovered Solvent be applied?
A: It is suitable for use in paint and coating industries, cleaning operations, chemical processing, and as a thinner in a range of manufacturing environments.Q: When is the best time to use this solvent for cleaning or thinning?
A: For optimal results, use the solvent during routine maintenance, equipment cleaning, or during paint and coating application processes that require quick evaporation and a clean finish.Q: What is the process for ordering and receiving samples?
A: You can request a sample during your inquiry. Upon approval, samples are promptly dispatched as per your requirement, ensuring you can evaluate the product before placing larger orders.Q: Is the product certified and how is it transported?
A: The solvent complies with relevant industrial standards and certifications, and is dispatched as dangerous goods using authorized transport services to ensure safe and timely delivery.
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Grade Chemical Category
99% Industrial Grade Isopropyl Alcohol IPA
Minimum Order Quantity : 100 Kilograms
Molecular Formula : C3H8O
Ph Level : ~7 (neutral)
Refractive Rate : 1.377 (20C)
Chemical Name : Isopropyl Alcohol
Boiling point : 82.6C
99% Industrial Grade Methylene Dichloride
Minimum Order Quantity : 100 Kilograms
Molecular Formula : CH2Cl2
Ph Level : Neutral
Refractive Rate : 1.424 (n20/D)
Chemical Name : Methylene Dichloride
Boiling point : 39.6 C
99% Industrial Grade MTBE Chemical
Minimum Order Quantity : 100 Kilograms
Molecular Formula : C5H12O
Ph Level : Neutral
Refractive Rate : n20/D 1.369
Chemical Name : Methyl tertbutyl ether
Boiling point : 55.2C
99% Industrial Grade Chloroform
Minimum Order Quantity : 100 Kilograms
Molecular Formula : CHCl3
Ph Level : Neutral
Refractive Rate : n20/D 1.445
Chemical Name : Chloroform
Boiling point : 61.2C

 Send Inquiry


3RD FLOOR, BLOCK - G, POCKET - 4, H.NO - 138 & 139, Guru Nanak Dev Road, Ryan International JR School, Rohini Sector 11, Delhi - 110085, India

Mr. Virendra Patel
(Proprietor)
Mobile :08071790308
 Send Inquiry
 Send SMS

Developed and Managed by Infocom Network Private Limited.
